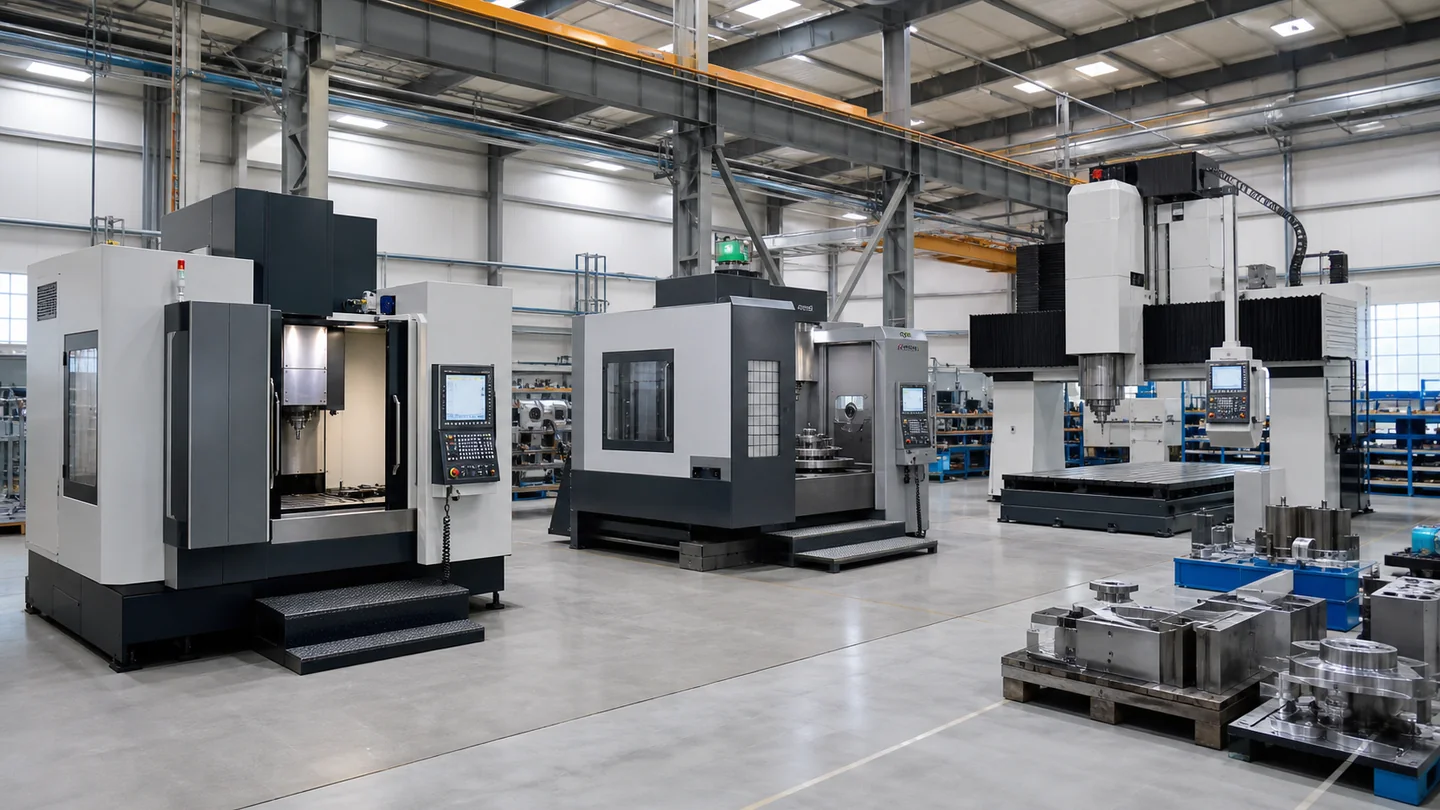
Choose a vertical, horizontal or gantry machining center by starting with the workpiece and the complete production route. Vertical machines offer open access and familiar setup for general work. Horizontal machines make several sides accessible and tend to manage chips well in production cells. Gantry machines provide an open, supported working area for large or heavy components. None is the default best choice.
A practical comparison
| Machine layout | Often a good fit for | Question that changes the decision |
|---|---|---|
| Vertical machining center | Mixed work, plates, molds and parts loaded from above | Can every required face be reached without too many reclamps? |
| Horizontal machining center | Multi-side production, pallet systems and work where chip evacuation matters | Will fixtures, pallets and tool capacity support the planned part family? |
| Gantry machining center | Large plates, frames, molds and heavy workpieces | What is the usable space after fixtures, guards, tool approach and probing are included? |
Work from the cutting envelope, not the brochure envelope
Machine travel is not the same as usable part capacity. A vise, tombstone, rotary table or angle head consumes space, and the spindle nose still needs a safe approach path. On a horizontal machine, the part may sweep through a much larger volume as the pallet indexes. On a gantry, cross-rail and ram geometry can limit access to tall features.
A reliable check uses the 3D part, fixture, holder and representative tools in one layout. It should include the loading path as well as the cutting positions. This catches a common buying error: a part fits inside the nominal travels but cannot be loaded, indexed or reached as planned.
Let the process narrow the choice
- Map the operations. Mark every machined face, critical datum and feature that needs a particular tool angle.
- Define the part family. Record the smallest and largest blanks, material range, mass, batch size and expected changeover frequency.
- Build a fixture concept. Check clamp access, distortion risk, chip traps and probe access before selecting options.
- Estimate the whole cycle. Include loading, probing, tool changes, indexing, chip clearing and inspection rather than cutting time alone.
- Test the factory constraints. Confirm floor space, foundation, lifting, electrical supply, air, coolant handling and operator access.
Two trade-offs buyers sometimes miss
A horizontal machine may reduce handling but require more investment in fixtures and pallets. A gantry may solve the size problem while increasing attention to foundation, loading and long-tool behavior. A vertical machine may be easier to operate yet create extra setups for a part with features on four sides. These are process costs, not defects in a machine type.
Shortlist a layout only after the supplier can place the actual part and fixture inside it and explain the proposed operation sequence. The CNC Tech machine range covers several layouts; use the comparison to identify a family, then request an application review for the final configuration.