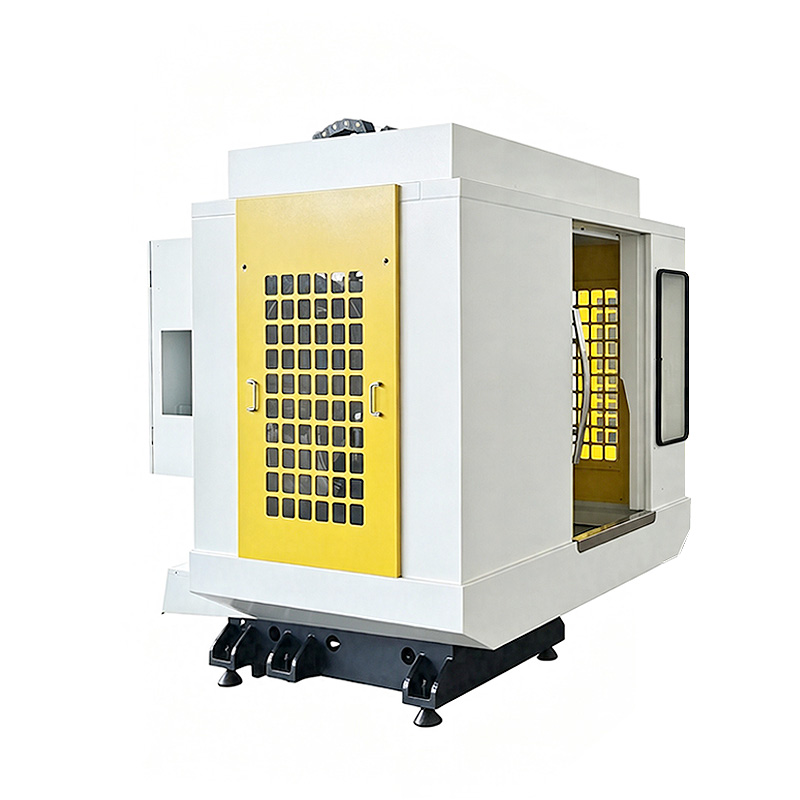
In a drill tap center vs VMC decision, choose the drill-tap machine when compact parts, frequent tool changes, drilling, tapping and lighter milling dominate. Choose a VMC when the work needs broader envelope, larger tooling, heavier or more varied cutting and greater process flexibility. The dividing line comes from the operation list, not the machine name.
Where a drill-tap center is a strong fit
Drill-tap centers are commonly arranged for quick axis and tool-change response with compact tooling. Housings, plates and small multi-hole parts can benefit when the magazine covers the job and milling remains within the spindle’s intended duty. Their smaller working area can also suit dense cells or automation, provided service and material flow still fit.
Where a VMC provides more margin
A VMC generally serves a wider range of part sizes, holder interfaces and cutting operations. It may be the safer platform when the process includes larger face mills, deeper steel removal, long tools or fixtures that consume significant clearance. Configuration varies widely, so these points must be confirmed on the exact models being compared.
| Decision factor | Drill-tap center tendency | VMC tendency |
|---|---|---|
| Primary work | Hole making and lighter milling | General and heavier milling mix |
| Part envelope | Compact setups | Broader range, model dependent |
| Tool strategy | Fast changes with a focused tool set | More varied or larger tools |
| Future flexibility | Efficient inside a defined process | Useful when job mix is uncertain |
Compare with the same part and fixture
Time loading, cleaning, probing, cutting and tool changes separately. Use identical material and equivalent tools. Inspect the features that drive acceptance. A faster dry cycle can be misleading if one machine requires a second setup or manual tool exchange.
Watch for middle-ground configurations
Spindle, magazine, rotary and automation options can move a specific model away from the typical category. Obtain the power and torque information, tool restrictions and loaded envelope for each offer. Decide from those facts rather than assuming every VMC is rigid or every drill-tap center is fast on the customer’s part.
CNC Tech can compare both routes from a common cycle and tooling sheet. That makes the recommendation traceable to production needs and exposes where a sample test is necessary.
Compare real configurations: review the T7S drill-tap center beside the VMC1165 vertical machining center.