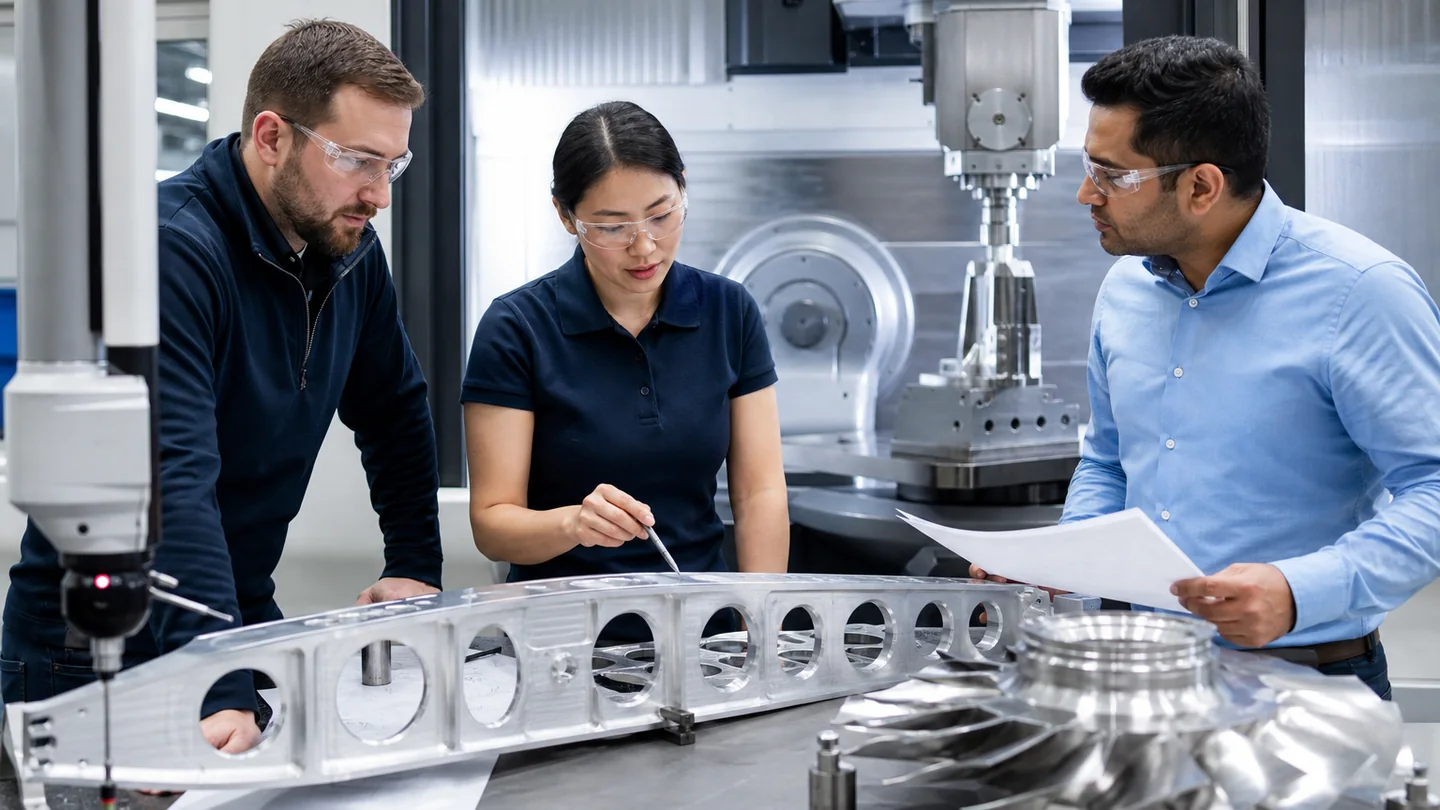
A 5 axis CNC for impellers must provide collision-free access between blades while controlling the relationship of hub, blades and bore. The part diameter alone is not enough to choose a machine. Blade spacing, depth, tool and holder reach, rotary layout, fixture, CAM strategy and inspection method all shape the practical requirement.
Start with the complete impeller model
Provide the raw blank, finished geometry and stock allowance. Mark splitter blades, narrow passages, leading and trailing edges, hub features and balance-related surfaces. Add the intended fixture and spindle-side holder. A kinematic study should check both cutting poses and safe entry or exit between blades.
Match operations to their risk
| Operation | Main concern |
|---|---|
| Blank preparation | Stable datum and clamping |
| Channel roughing | Chip evacuation, tool load and collision margin |
| Blade finishing | Tool contact, deflection and smooth orientation |
| Hub and bore work | Relationship to the rotary datum |
| Inspection | Accessible, defined comparison to requirements |
Control the programming chain
The CAM software, postprocessor, machine kinematics and CNC options must agree. Use actual tool assemblies and machine solids in simulation. Preserve the post version with the released program and define who revalidates it after a software, control or machine-configuration change.
Plan for thin-feature behavior
Blade deflection can change with toolpath direction, stock distribution, tool reach and material. Develop the roughing and finishing sequence together. A sample should use representative geometry and material; an open test surface does not reveal access or flexibility inside a narrow channel.
Agree on verification before cutting
Define the datums, measurement equipment and surfaces included in acceptance. Machine probing can support setup and in-process checks, but final verification must follow the drawing and quality plan. Rotary calibration and tool data should be recorded with the trial.
Send CNC Tech the impeller model, blank, material, fixture concept and CAM platform. A feasibility review can then identify the limiting blade passage and prove the proposed five-axis layout against it.
Five-axis process resources: read the setup-reduction guide and inspect the U650 five-axis machine.