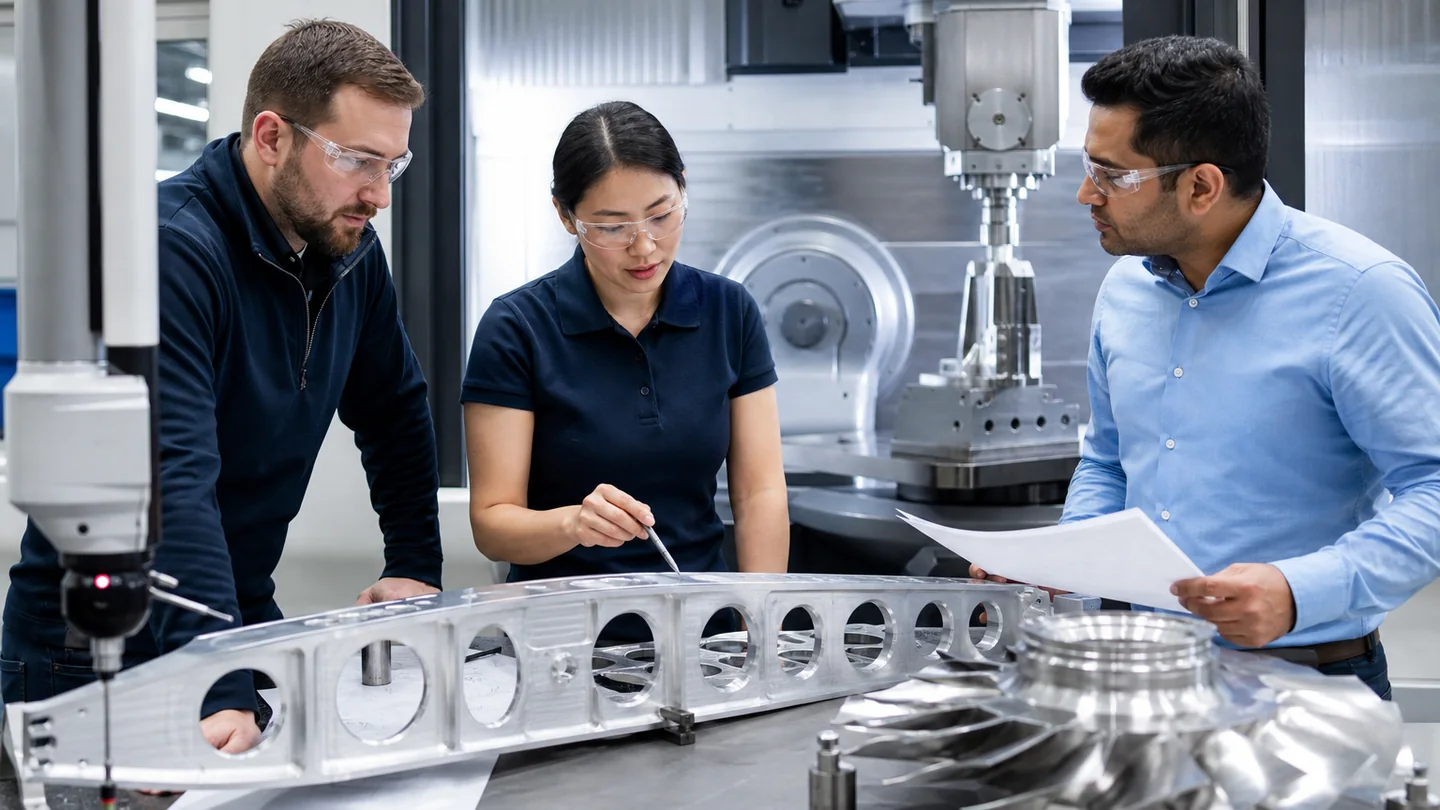
A CNC machine for aerospace components must be selected within the customer’s approved manufacturing and quality system. Aerospace parts range from small precision housings to thin structural components and complex rotating forms, so no machine category is correct for the sector as a whole. The drawing, material, process controls and verification plan define the equipment need.
Classify the actual component
Record stock form, alloy, heat-treatment state, geometry, wall thickness and datum scheme. Identify features requiring one-setup relationships, long reach or changing tool orientation. A rigid three-axis machine may suit accessible prismatic work, while five-axis equipment may reduce setups for complex surfaces. Large structures can require a gantry layout and a detailed support strategy.
Keep compliance claims inside the approved scope
A machine purchase does not by itself establish aerospace qualification. The manufacturer remains responsible for customer approvals, special-process controls, calibration, traceability, inspection and documented procedures. Ask the machine supplier for evidence within its scope and avoid treating a general industry statement as approval for a particular part.
| Process input | Machine or cell implication |
|---|---|
| Material and removal volume | Spindle duty, tooling, coolant and chip management |
| Thin walls | Workholding, cutting sequence and in-process checks |
| Complex orientation | Rotary envelope, postprocessor and calibration |
| Traceability | Program, offset, tool and inspection record controls |
| Acceptance feature | Defined sample and measurement method |
Control the digital thread
Released model and drawing revisions, CAM files, postprocessor version, machine setup and inspection program must remain aligned. Define authorization for program changes and how offsets and tools are recorded. Connectivity can support collection, but it does not replace process ownership or validated records.
Demonstrate the representative risk
Use a test that reflects difficult material, reach, wall behavior or multi-axis relationship. Agree on stock, tools, program and inspection before the test. Retain the result as evidence for factory and site acceptance where appropriate.
Share non-controlled application data that is authorized for supplier review with CNC Tech. A useful proposal will state assumptions and limits rather than imply blanket aerospace approval.
Aerospace application context: review the aerospace machining solution and the structural-parts application case.