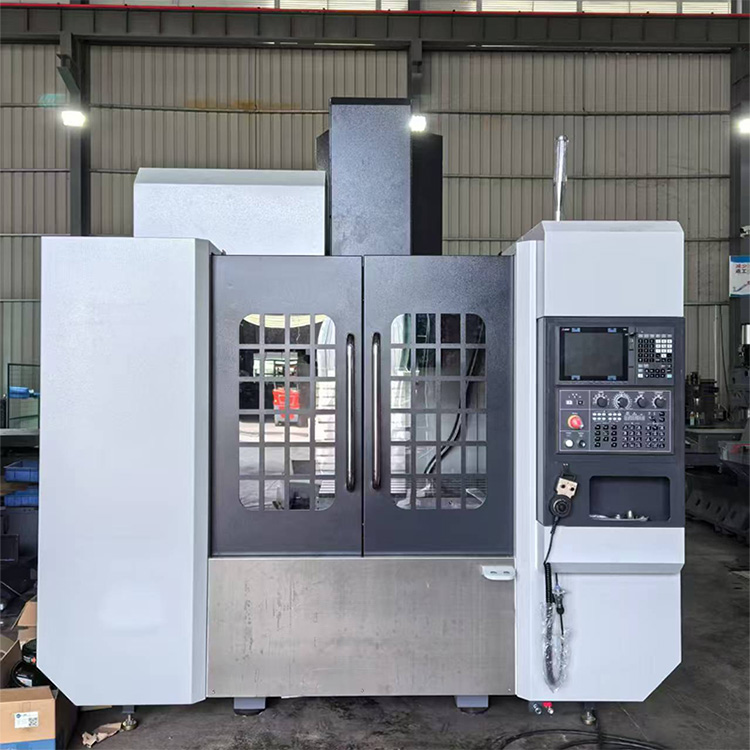
A vertical machining center with a pallet changer allows setup or unloading on one pallet while another pallet is in the machining area. It can reduce spindle waiting when external handling is a meaningful part of the cycle. It does not automatically improve output if cutting time is short, fixtures are slow to prepare or the next part is not ready.
Calculate the idle time the pallet system can remove
Measure door-open time, cleaning, part removal, fixture loading, datum confirmation and restart. Compare that external work with the machining cycle. If preparation routinely finishes before cutting, overlapping the tasks may help. If it takes longer, the pallet changer simply moves the waiting point.
Check the complete pallet assembly
- Part, fixture, clamps and tombstone mass must stay within the approved pallet load.
- The tallest clamp and longest tool must clear during exchange and machining.
- Locating surfaces need a cleaning and inspection routine.
- Programs, offsets and work identification must follow the correct pallet.
- Guarding and operator access must cover setup and automatic exchange states.
| Production pattern | Likely value | Planning concern |
|---|---|---|
| Repeated part with long cutting cycle | Good opportunity to prepare the next load offline | Fixture durability and inspection frequency |
| High-mix work | May reduce changeover if pallets keep dedicated fixtures | Program and offset control |
| Very short operations | Exchange time may consume the expected gain | Use a measured cycle study |
| Unattended periods | Can support a small queue | Tool life, chip control and fault recovery |
Specify recovery before automatic operation
Document what happens after a power interruption, incomplete exchange, probe rejection or missing part. The controls must preserve pallet identity and prevent an uncertain setup from resuming without verification. Maintenance access to the changer also belongs in the safety review.
A pallet study needs the real handling sequence and fixture concept. Provide those details with the target cycle so CNC Tech can determine whether a pallet-changing VMC removes a real bottleneck or adds equipment without enough return.
Planning references: use the CNC automation guide to define pallet control and review CNC Tech application engineering for the project workflow.