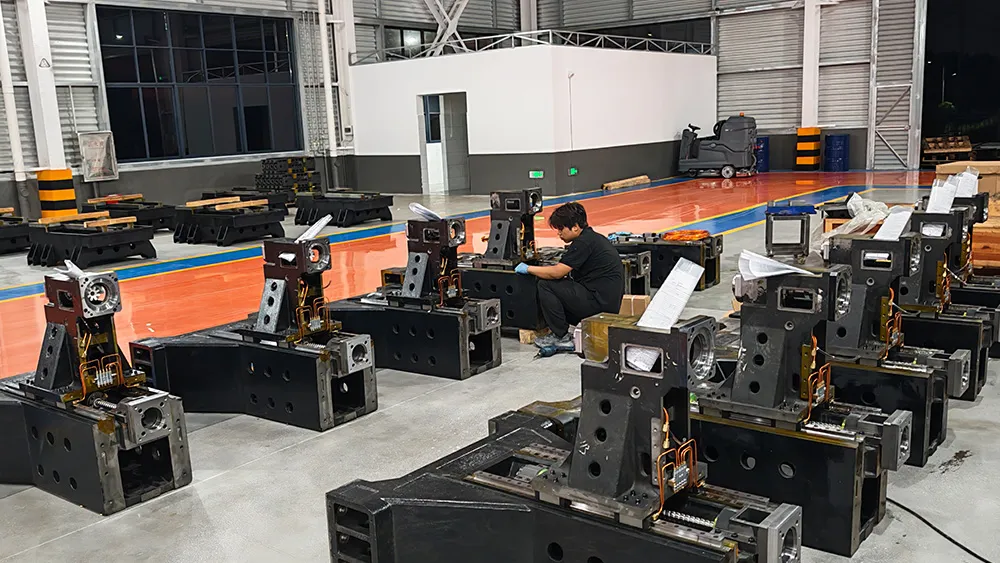
A gantry machining center for large parts is chosen successfully when the entire loaded setup, operation sequence and handling route are considered together. A long or wide component can fit the nominal table yet exceed usable clearance after supports and clamps are added. It may also need repositioning if the spindle cannot access all features in the required relationship.
Model the real setup at its worst orientation
Use a solid model containing the raw part, finished part, fixture, clamps, lifting points, probes and representative tools. Check column clearance and bridge height through the full program, not only at home position. For flexible weldments or plates, show support locations and where cutting force may cause deflection.
| Planning item | Decision it supports |
|---|---|
| Mass and center of gravity | Table capacity, loading method and support distribution |
| Datum and critical relationships | One-setup strategy and probing sequence |
| Feature access | Vertical head, angle head or rotary-head requirement |
| Material and chip form | Spindle duty, conveyor and coolant system |
| Final measurement | Machine checks, external inspection and acceptance |
Control distortion rather than discovering it late
Large parts may contain residual stress or move as stock is removed. Plan roughing, relaxation if required by the customer’s process, re-datum and balanced finishing. Probing can locate features and monitor change, but it cannot make an unstable part rigid. Workholding and cutting order deserve the same review as the machine.
Make loading and service safe
Confirm crane coverage, sling space, table access and an unobstructed path into the enclosure. Define where operators can clean, inspect and change tools. Maintenance space around way covers, chip equipment and cabinets must remain available after the machine is placed.
Use staged acceptance
Factory tests establish the assembled machine before shipping; site tests confirm geometry after foundation work, transport and installation. State which tests repeat, the temperature and warm-up rules, and who provides instruments. A representative part test is valuable only when the setup and measurement are reproducible.
CNC Tech can evaluate a large-part application from the model, setup mass, fixture plan and critical tolerances. This information makes it possible to identify clearance or process risks before the machine configuration is fixed.
Large-part references: view the 8080 gantry machine page and CNC Tech’s gantry production capability.