Editorial answer: A CNC supplier or manufacturer should be evaluated through traceable engineering and production evidence, not catalogue language alone.
Verify who owns application engineering, assembly checks, inspection records, change control, shipment release and after-sales escalation.
Quick answer
best drilling tapping center company should be judged by hole and thread demand, milling load, spindle and taper, tool changes, chip evacuation, fixture access and acceptance evidence.
- Define the representative part and complete fixture envelope.
- Normalize included, optional and excluded scope.
- Prove the process with a named test and recorded measurements.
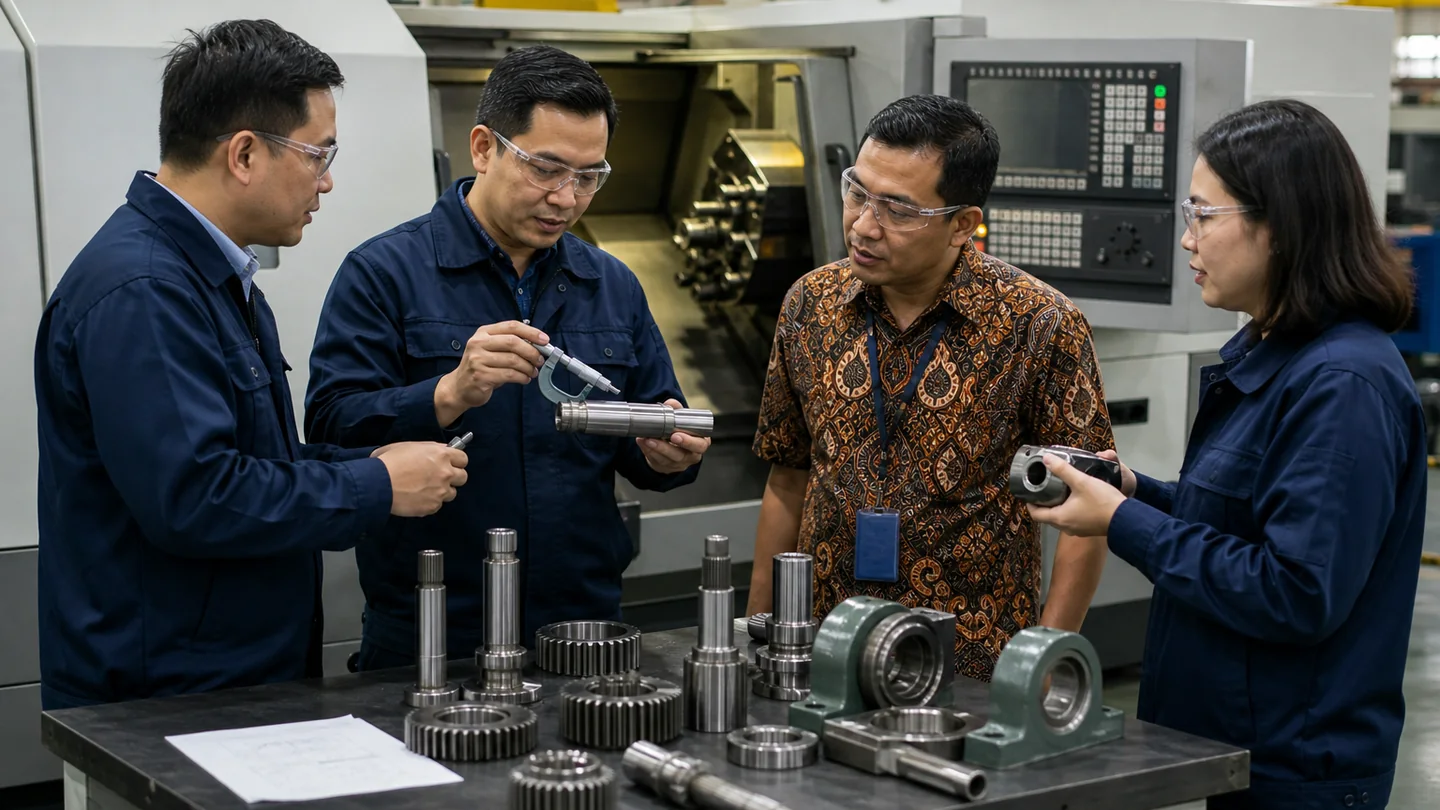
What does “best drilling tapping center company” mean?
The term describes a buying intent, not a universal machine specification. Drill-tap centers vary in travel, spindle torque, tapping method, tool capacity, axis acceleration and table loading. A credible proposal states the exact configuration and its process assumptions.
Define the process first
Provide material, stock condition, hole count, diameters, thread sizes, depths, milling features, tolerances, surface needs, batch size and target cycle. Add clamps, fixture datum, longest tool and safe approach to the envelope. Note coolant, chip behavior, probing and inspection requirements.
Compare quotations on one scope
| Area | Specify | Evidence |
|---|---|---|
| Machine | Travels, table load, spindle, taper and control | Approved option list |
| Tools | Magazine, holders, tapping tools and change sequence | Tool list and duty assumptions |
| Process | Fixture, coolant, chip removal, probing and program | Cycle study or test plan |
| Delivery | Freight, installation, training, warranty and service | Responsibility matrix |
Review the U650 Bridge-Type 5-Axis Machining Center as a product starting point; final capability belongs in the signed quotation.
Verify with a representative test
Agree on material, tools, fixture, program revision, warm-up, measurement method and acceptance limits. Record thread quality, hole position, surface result, cycle elements and operator actions. Machine checks and part inspection answer different questions, so retain both.
FAQ
What makes a drill-tap center productive?
Balanced spindle duty, fast and repeatable tool changes, stable tapping, effective chip evacuation and a fixture that supports the whole cycle.
Should I compare speed alone?
No. Tool changes, approach moves, chip clearing, probing, loading and inspection can dominate the real cycle.
Can catalogue accuracy guarantee my part?
No. Workholding, tools, material, temperature, program and measurement also affect results.
Conclusion
A sound best drilling tapping center company decision is traceable from part requirements to configuration, quotation and acceptance. Keep assumptions visible and choose the simplest system that proves the required work.