The vertical-versus-horizontal decision is mainly about access, chip flow, workholding, setup count and production pattern. A VMC is often simpler to load and prove out; an HMC can provide multi-face access and pallet-oriented production when the part family justifies it.
For prismatic parts, housings, manifolds, fixtures and production components, a useful proposal explains the process assumptions in plain language. It also separates standard equipment, optional equipment and buyer-supplied items. That discipline prevents the common mistake of choosing by machine prestige instead of the number of operations, setups and required output.
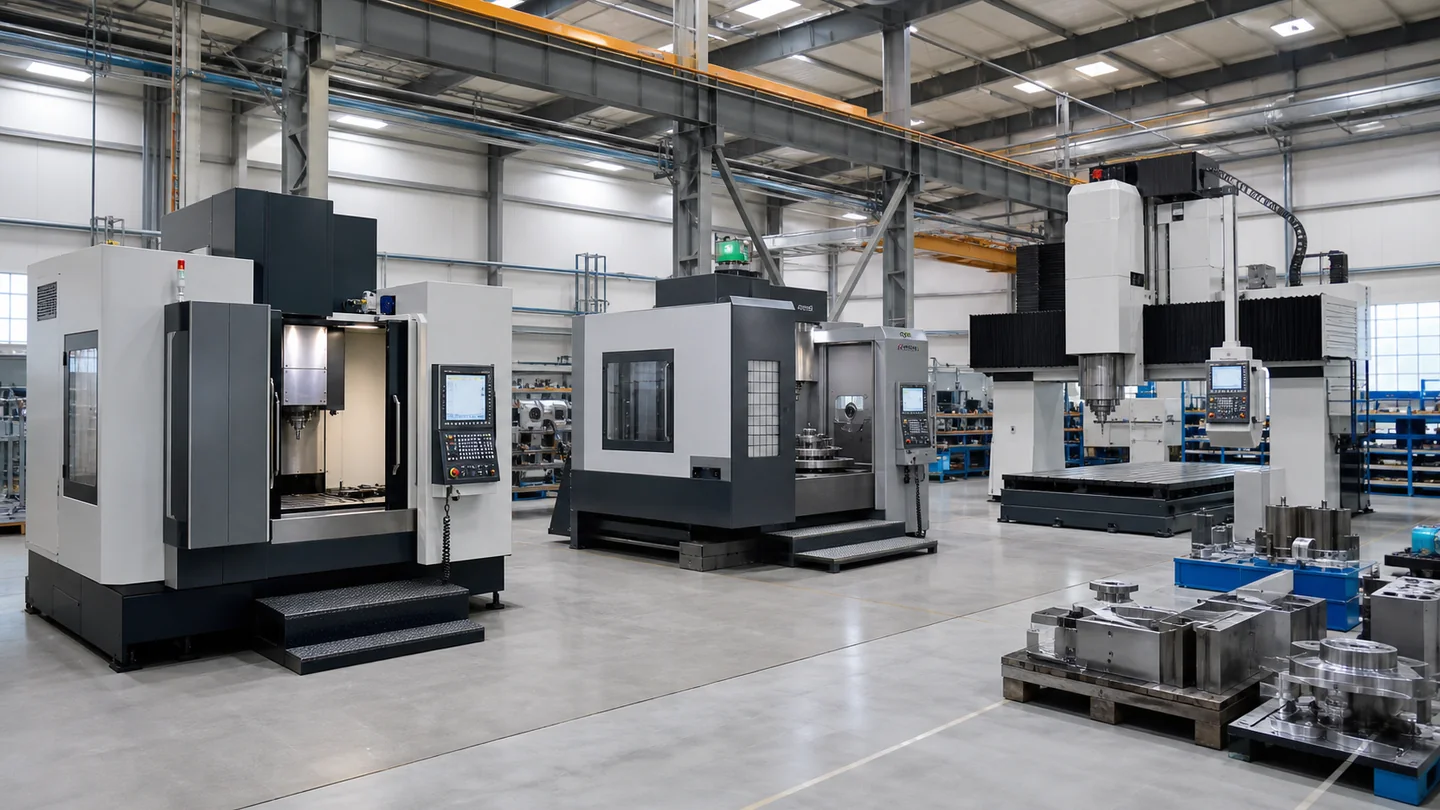
What does “vertical vs horizontal machining center” mean in a buying project?
Vertical and horizontal machining centers use different spindle orientations and workholding strategies. Neither layout is universally better; the more suitable choice is the one that reaches the required faces with fewer risky handlings at the needed production rate.
The phrase is useful for discovery, but it is not a complete specification. Model names and category labels vary among suppliers. Always ask for a dimensional drawing, installed option list and explicit statement of what the quoted machine will and will not do.
Define the process before comparing machines
Start with the hardest representative part, not an average part. Record material, incoming stock, finished dimensions, critical tolerances, surface requirements, annual volume, batch size and target working pattern. Add the fixture, clamps, toolholders and tool approach to the part envelope. A nominal travel value can look adequate while the real setup collides or loses clearance.
Next, sketch the process route. Identify datums, orientations, roughing and finishing tools, hole and thread requirements, deburring, inspection and material handling. This reveals whether the proposed architecture reduces setups or simply moves complexity into fixtures and operator work.
A comparison table for vertical vs horizontal machining center
| Area | Input to provide | Evidence to retain |
|---|---|---|
| Feature access | Faces reached per setup and tool approach limitations | Record the agreed value and the evidence used to verify it. |
| Workholding | Fixture simplicity, tombstone opportunity and changeover effort | Record the agreed value and the evidence used to verify it. |
| Chip behavior | Where chips collect and how coolant removes them | Record the agreed value and the evidence used to verify it. |
| Production pattern | Batch size, repeat work, pallet use and operator loading | Record the agreed value and the evidence used to verify it. |
| Economics | Complete cell cost, setup hours, tooling and floor requirements | Record the agreed value and the evidence used to verify it. |
What a comparable quotation should include
Ask each supplier to return the same compliance matrix. It should identify the exact machine, CNC control, spindle and taper, tool capacity, coolant and chip equipment, guarding, electrical standard, manuals, documentation language, packing, freight responsibility, installation, training, warranty and acceptance. Mark every line as included, optional, excluded or buyer supplied.
Do not force a supplier to promise a cycle time from an incomplete drawing. A credible estimate states its assumptions: material condition, stock allowance, tools, workholding, toolpath, inspection method and operator actions. If production output is important, ask for a time study or witnessed test using an agreed representative program.
For a concrete starting point, review the VMC1165 Vertical Machining Center. Treat the published page as an application overview; final capacity, performance and included options belong in the approved quotation and machine specification.
Verify capability with evidence, not adjectives
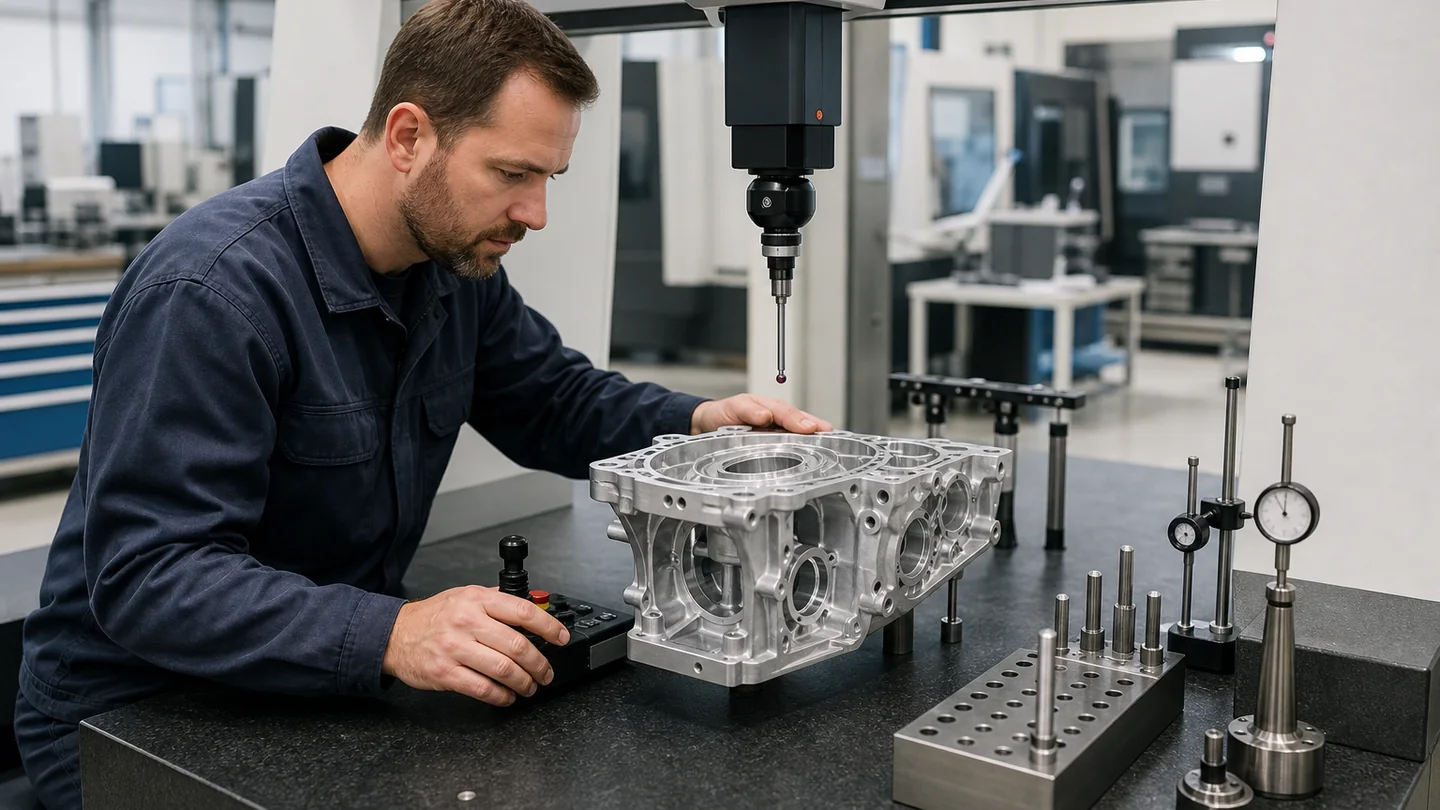
Words such as high precision, heavy duty and high speed need a test condition. Define the measurement method, instrument, machine warm-up, environmental condition and reporting format. For the workpiece trial, agree on material, drawing revision, fixture, tools, quantity, inspection points and who owns the resulting program and records.
For a remote evaluation, request dated images or video tied to the machine serial record, along with inspection documents and a live review of the control and installed options. Before shipment, close every open item in a signed acceptance report. After delivery, repeat the agreed site checks once the machine is leveled and thermally stable.
Plan installation and support before the purchase order
Confirm the transport route, door and ceiling clearances, crane or forklift plan, foundation, electrical supply, air, coolant handling, networking and local safety requirements. Assign responsibility for rigging, leveling, startup, operator training and post-installation acceptance. A technically suitable machine can still lose weeks if the site scope is left until shipment.
Support should be written as a process: first response, remote diagnosis, escalation, parts identification, shipment route and warranty decision. Ask which items are stocked, which come from component partners and what information your maintenance team must provide when opening a service case.
Frequently asked questions
What information should I send first?
Send a representative part drawing, material and stock condition, critical tolerances, required surfaces, annual volume, batch size, desired automation level and site electrical standard. A fixture concept and current cycle data make the review more useful.
How should I compare two proposals?
Normalize both proposals into one compliance table. Compare installed configuration, options, exclusions, acceptance, delivery responsibility, training, warranty and service—not only the model name and base price.
Can a catalogue accuracy value guarantee my part?
No. Machine checks describe the machine under a stated method; part results also depend on workholding, tools, program, material, temperature and measurement. Use both machine tests and an agreed representative part.
What is the safest next step?
Prepare a controlled RFQ and ask shortlisted suppliers to explain their assumptions. Resolve technical gaps before price negotiation, then attach the approved specification and acceptance plan to the purchase agreement.
Conclusion
A sound vertical vs horizontal machining center decision is traceable from part requirements to configuration, quotation and acceptance. Keep the process evidence together, insist on clear responsibility and choose the simplest system that can prove the required work.