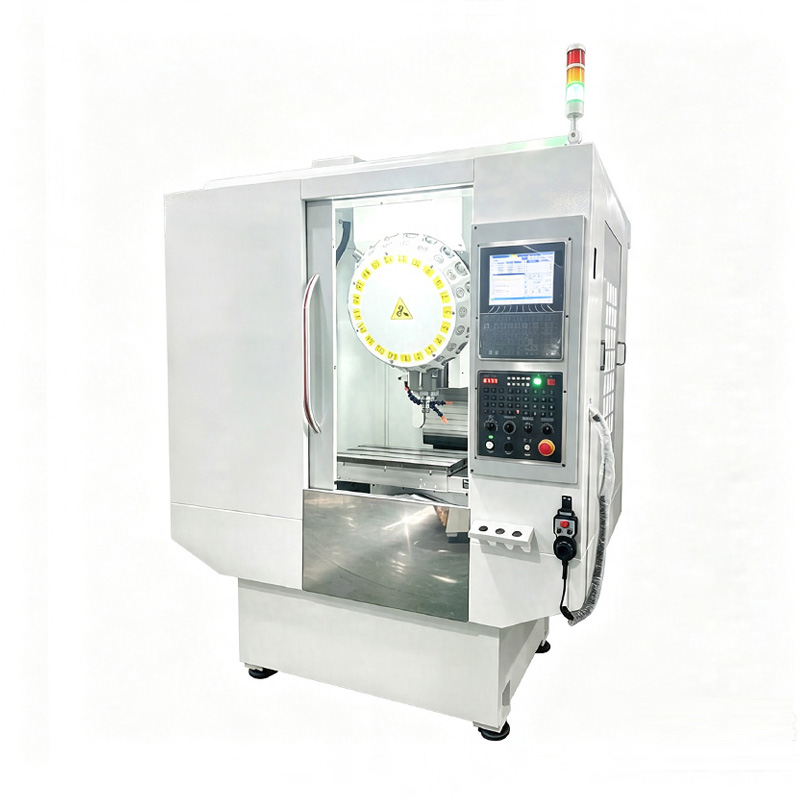
A 5 axis drill tap center combines the rapid tool-change and hole-making focus of a drill-tap machine with two rotary motions. It is most valuable for compact parts whose holes, threads and light milled features appear on several faces. It is not a substitute for a heavier machining center when the process is dominated by large cutters or sustained roughing.
Count the setups the rotary axes can remove
Group features by tool direction and note which relationships are difficult to preserve after reclamping. If indexing exposes side holes and faces in one fixture, the machine may reduce handling and accumulated datum error. If nearly all work is vertical, a standard drill-tap center with a simpler fixture may be the more economical route.
Check the part at every index
Add stock, fixture, clamps, probe and actual holders to the machine model. Verify clearance during tilt, rotation, tool change and safe retract. The rotary table’s approved load must cover the entire setup, including its center-of-gravity condition. Small parts can still create interference when arranged in a multi-part fixture.
| Process question | Selection consequence |
|---|---|
| Are operations mainly drilling and tapping? | Supports a fast, compact drill-tap architecture |
| Is heavy stock removal required? | Review a machining center with greater cutting duty |
| Do side features share tight locations? | One indexed setup may reduce transfer risk |
| Is unattended production planned? | Tool life, chip removal and fault recovery become central |
Build the complete tool and chip plan
Count drills, taps, thread mills, probes and finishing cutters to confirm magazine capacity. Through-tool coolant may be needed for certain holes, but the requirement depends on depth, diameter and material. Tilting can help chips leave a bore or trap them elsewhere, so assess each critical orientation.
Validate angled relationships
A sample should include a feature that uses the rotary axes and an inspection method for its location or angle. Keep rotary calibration and fixture datum checks in the maintenance plan. A vertical test plate cannot prove the five-axis part of the investment.
Send CNC Tech the part model, hole schedule, fixture and operation times. That evidence makes it possible to compare a five-axis drill-tap center with a conventional machine and additional setups.
Relevant machine options: compare the AC U400 five-axis drill-tap center with the broader machine selection guide.